Skip to Content

TRANSFORMER APPLICATION

Transformers for Manufacturing Plants

Match transformer selection to how the production equipment actually operates. Motor starts, variable-speed drives, welding cycles and changing shifts create different requirements from a simple total of installed machine power. Share the machine data, operating pattern and supply arrangement so the enquiry can separate transformer duty from plant-wide power-quality, protection and process-control decisions.

Discuss Your Project
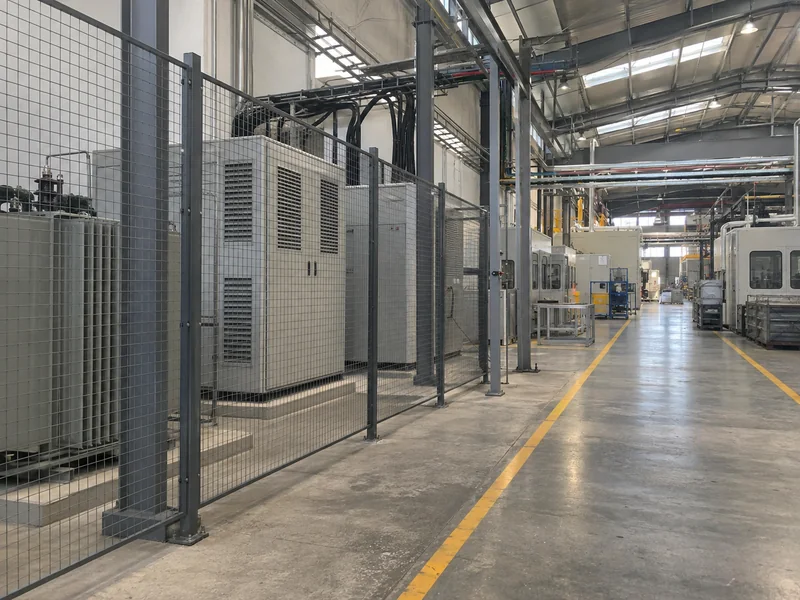
Electrical equipment behind a mesh partition beside the service aisle of a manufacturing hall

Start with your project task

Supply motor-driven production equipment

Compressors, pumps, conveyors and large process motors may share a supply with sensitive controls or other running machinery. Starting conditions can be different from normal production demand. The motor's rated power alone does not describe the current and voltage conditions during acceleration.

Send these inputs
Motor list and manufacturer data, largest motors, starting methods and current information, starting frequency and sequence, already-running loads, acceptable supply conditions for connected equipment, single-line diagram and available source data.
Review and coordination
Identify the transformer duty and the motor-starting questions that need a network assessment. Capacity and impedance must be coordinated with the upstream supply, connected loads and protection requirements. Do not prescribe a lower impedance or larger unit without considering those system interfaces.
Expected output
A motor-load enquiry brief with required equipment data, starting scenarios and the system-study inputs to resolve before the transformer configuration is confirmed.
Discuss This Task

Define drive, rectifier and cyclic process duty

A production area may combine variable-frequency drives, rectifiers, welding supplies and other cycling machinery. Equipment labels and quantities do not fully describe the current drawn from the supply. Different drive arrangements and operating cycles can lead to different transformer review requirements.

Send these inputs
Drive and rectifier datasheets, input-current or harmonic information where available, welding or process duty cycles, simultaneous operation, load measurements, existing filters or power-factor equipment, supply diagram and applicable power-quality requirements.
Review and coordination
Separate the transformer's ability to carry the specified load from any measures intended to reduce distortion elsewhere in the plant. Record missing spectrum or duty information and identify the required assessment. A harmonic-tolerant transformer is not automatically a complete filtering solution.
Expected output
A documented load basis for the equipment enquiry, with thermal-duty questions, power-quality assessment needs and any separately specified mitigation interfaces clearly identified.
Discuss This Task

Add a production line or extend operating shifts

A new line or longer working day can change both peak demand and the time spent at high load. Existing spare nameplate capacity is not the same as a complete assessment of the changed process. Expansion planning should use the operating pattern, not only an allowance added to today's equipment list.

Send these inputs
Measured demand and operating records where available, existing transformer data, added machinery and starting requirements, proposed shift schedule, process coincidence, expected growth stages, installation space and the plant's maintenance or outage constraints.
Review and coordination
Compare present and future duty, including sustained loading, repeated peaks and lightly loaded periods. Identify what the designer must review in the supply arrangement and compare offered losses under consistent conditions. Distinguish confirmed expansion from provisional future demand.
Expected output
A staged duty brief for comparing additional or replacement equipment, with capacity assumptions, loss-evaluation inputs and unresolved network or installation questions.
Discuss This Task

Conditions that affect configuration

Motor starting, voltage performance and system coordination

Starting current can produce a voltage dip through the supply impedance and affect other connected equipment. The relevant assessment includes more than the transformer: source strength, feeders, running loads, starting equipment and motor requirements also matter.

Information to provide: Provide starting data, sequence, acceleration or duty information where available, source and feeder details, and the equipment's permitted voltage conditions. Ask the responsible designer to coordinate starting performance with fault levels and protection. Transformer energization inrush and motor starting are separate events and should not be merged into one assumed current multiplier.

Nonlinear current, cyclic loads and harmonic tolerance

Nonlinear loads can add heating and distortion concerns, while cycling changes the time pattern of demand. Neither an average current nor the number of drives is a complete specification. A proposed thermal capability must be tied to the actual load information.

Information to provide: Supply the relevant current spectrum or manufacturer data, duty cycle, simultaneous loading, phase balance and available measurements. Identify the power-quality assessment point and required criteria. Include existing capacitor banks or filters in the system review, rather than adding or changing mitigation equipment based only on a transformer label.

Operating hours, losses and future production duty

Loss comparison should reflect how the equipment will be used. No-load loss remains while the transformer is energized, and load-related loss changes with demand. A single efficiency figure or an oversized capacity does not establish the lowest operating cost for every shift pattern.

Information to provide: Provide expected energized hours, load profile, confirmed expansion stages and any owner-specified loss evaluation method. Compare no-load and load-loss data at consistent reference conditions for the offered configurations. Keep the purchase price, installation implications and operating assumptions visible; do not use an unverified saving percentage or payback promise.

Factory environment, cooling and service access

An electrical room beside a clean production line can have different conditions from a hot, dusty or humid process area. Equipment protection, cooling paths and maintenance access must suit the actual location. Indoor placement alone is not an environmental specification.

Information to provide: Describe ambient temperature, altitude, dust, moisture, oil mist or corrosive exposure where relevant, room ventilation, cable or busbar entry and maintenance access. Confirm the proposed cooling and monitoring interfaces, auxiliary supplies and applicable enclosure requirements. Hazardous-area or hygiene requirements must be stated separately and reviewed for the actual installation.
Explore suitable product options

Oil-immersed transformers

Explore liquid-filled equipment for the proposed plant distribution duty. Review loading, cooling, losses, terminal arrangement and accessories together with the installation's fluid-containment, fire-safety and maintenance requirements. A factory application does not by itself confirm a special rectifier, furnace or welding-transformer design.

Review product range

Dry-type transformers

Explore dry-type equipment where the indoor or enclosed arrangement is appropriate. Confirm the actual process load, thermal basis, environmental requirements, ventilation, clearances and monitoring. Oil-free construction does not remove power-quality, cooling or maintenance considerations, and does not automatically establish cleanroom or hazardous-area approval.

Review product range

Documents by project stage

Machine-load and quotation basis

Collect the supply diagram, motor and electronic-load data, production cycle, site conditions and project specification. Identify missing measurements or machine information. Ask proposals to state the equipment duty, included accessories and documents, assumptions and deviations so offers can be compared without silently adopting different operating scenarios.

Stage: quotation

Equipment and production interfaces

Review configuration-linked rating, impedance, loss and cooling information with the responsible electrical designer. Coordinate terminals, general arrangement, ventilation and monitoring diagrams with the installation. Define the applicability of any load or harmonic assessment and test references; equipment documentation does not replace a complete plant network or process study.

Stage: design approval

Inspection and operating handover

Agree the applicable test and inspection records, identification, accessory checks and document revisions. Include approved drawings, installation and maintenance information, monitoring interfaces and any agreed operating limitations. The plant team should coordinate commissioning, protection and process restart under its own approved procedures; a factory test does not demonstrate uninterrupted production.

Stage: delivery

Scope and coordination

Transformer supply includes only the equipment, documents and services stated in the offer. Plant load studies, harmonic mitigation, fault and protection coordination, machine controls, room services and production-continuity arrangements are not automatically included. The responsible designers and operators confirm these interfaces. Existing overheating, trips or voltage complaints require qualified investigation; replacing a transformer is not a guaranteed diagnosis or remedy.

Questions before requesting a quotation

Can the transformer be selected from the total motor kW alone?

That is not a complete selection basis. Include voltage, actual loading, starting method and current, machine sequence, duty cycle and the other equipment already operating. The enquiry should identify both running and starting scenarios, with system performance assessed by the responsible designer.

Does a K-rated transformer remove harmonics from the plant?

No. A K-rating concerns the specified tolerance of harmonic-related heating; it is not, by itself, a harmonic-cancellation function. Any required distortion reduction needs its own assessment of the loads and network. Confirm both the transformer's duty and the scope of any separate mitigation.

What if harmonic measurements are not available yet?

Send the machine and drive datasheets, input-current information, quantities, operating cycles and existing supply arrangement. Mark measurements or study results as unavailable. This supports an initial technical enquiry while keeping any unverified load assumptions open, rather than inventing a harmonic level.

Is a plant supply transformer the same as a welding or rectifier transformer?

Not necessarily. Supplying a factory distribution board is different from serving a specialized process directly. State the equipment's role, connection and manufacturer requirements. Special-purpose designs need their own specification and confirmed supply scope; they should not be inferred from a general manufacturing application page.

Send your project requirements

Share the voltage, capacity, installation conditions and project specification. A document link is optional.

Request a Technical Discussion